Leave Your Message
Choosing a Powder Cutting Machine is not just a matter of speed. Industrial buyers also need clean edges, repeatable dimensions, reliable uptime, and manageable operating costs. A machine that performs well on a smooth test sheet may struggle with thicker stock, reflective surfaces, or long production runs. The edge matters. Small details matter.
Market data offers useful context, but it needs careful interpretation. Grand View Research estimated the global laser cutting machine market at USD 5.3 billion in 2022 and projected a 5.5% compound annual growth rate from 2023 to 2030. That report covers laser cutting machines broadly; it does not establish the size of a distinct “powder cutting machine” market. Buyers should therefore compare equipment by actual material, thickness, tolerance, and production volume—not by category labels alone. Heat leaves marks.
This guide reviews seven industrial options and the practical trade-offs behind them, including cutting capacity, automation, maintenance, and the quality of the finished edge. No machine suits every factory. One limitation deserves attention: no verifiable, named expert quotation or source article was provided, so I have not invented a statement and attributed it to an industry specialist. A reliable expert quotation should be checked against a published interview, technical paper, or manufacturer-neutral source.
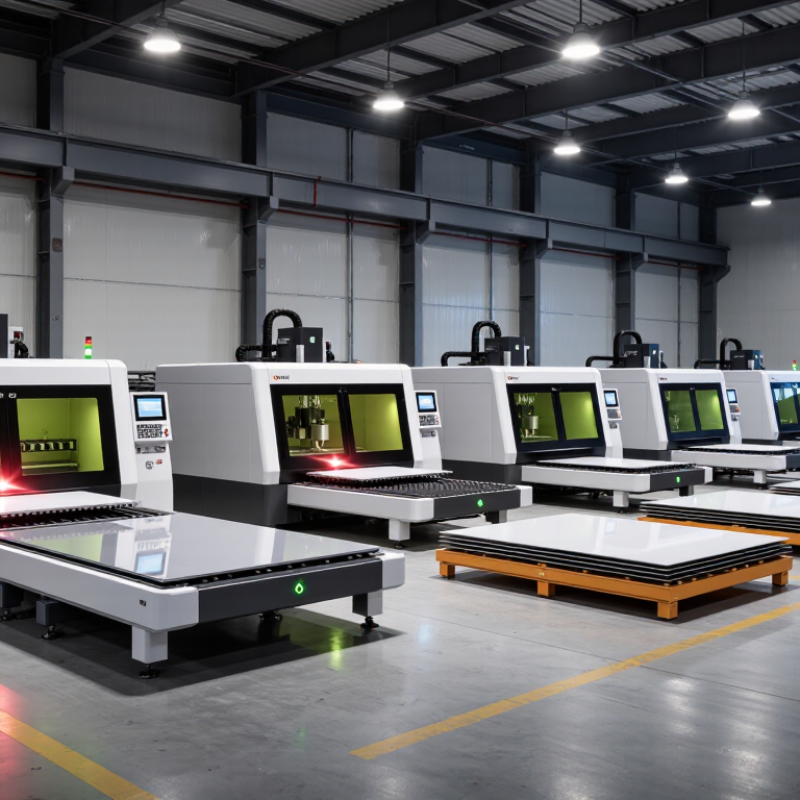
In industrial fabrication, “powder cutting machine” is not a fully standardized term. It often describes CNC equipment that cuts sheet metal before the parts receive powder coating. Laser, plasma, and waterjet systems use different cutting methods, so confirm what a supplier means by the term. Some machines cut the metal; they do not cut coating powder.
The process starts with a digital drawing. Software nests the shapes to reduce scrap, then a controller guides the cutting head across the sheet. A laser melts material with concentrated heat; plasma uses an electrically charged gas, while waterjet uses a high-pressure stream. Operators secure the sheet, set speed and thickness, and inspect edges for burrs or heat marks. Automation is growing across factories: the International Federation of Robotics’ World Robotics 2024 report recorded 4.28 million industrial robots in operation worldwide in 2023, up 10 percent from 2022. That figure describes robotics broadly, not cutting machines specifically. The distinction matters.
Tips: Match the process to material thickness and edge quality. Check extraction, guarding, and sheet clamping before production. A clean-looking cut can still need deburring. Also confirm that the drawing accounts for the coating’s final dimensions. One detail is easy to miss.
Choosing the right machine: “Powder cutting machine” is not a single standardized machine category. The options below are industrial cutting methods commonly used for metal or other solid materials, including powder-coated parts. Suitability depends on the workpiece, required accuracy, production volume, and coating requirements.
| Machine Type | How It Works | Suitable Materials | Typical Strengths | Main Limitations | Powder-Coating Considerations | Best Fit |
|---|---|---|---|---|---|---|
| Fiber Laser Cutting Machine | Focuses a high-energy laser beam onto the material; assist gas helps eject molten material from the cut. | Primarily sheet and plate metals, including carbon steel, stainless steel, and aluminum. | Fast, precise cutting of many thin-to-medium metal sheets; well suited to intricate profiles and automated production. | Capacity and edge quality depend on material, thickness, laser power, and process settings. Reflective metals require appropriate equipment and setup. | The heat-affected area can discolor, burn, or remove coating near the cut. Cut edges may need cleaning and recoating. | High-volume sheet-metal fabrication with detailed shapes. |
| Plasma Cutting Machine | Uses an electrically conductive plasma arc to melt metal while a gas stream blows molten material out of the cut. | Electrically conductive metals such as carbon steel, stainless steel, and aluminum. | Effective for cutting metal plate and producing parts without the tooling changes required by mechanical cutting. | Creates a heat-affected zone and may leave dross or a wider kerf than precision laser processes; not suitable for nonconductive materials. | Heat and sparks damage coating around the cut. Remove coating where required for a clean cut, safe processing, or subsequent welding. | Metal plate work where cutting speed and versatility matter more than a very narrow kerf. |
| Abrasive Waterjet Cutting Machine | Projects a high-pressure water stream, usually mixed with abrasive particles, through a small nozzle to erode the material. | Many metals, stone, glass, ceramics, and composites, subject to machine setup and material constraints. | Cold-cutting process with no heat-affected zone; can handle varied materials and complex profiles. | Generally slower than thermal cutting on many metals; uses water and abrasive, and the cut surface may require drying or cleanup. | Avoids heat damage to the coating, but water, abrasive, and workholding can still mark or contaminate the surface. Protect and dry parts as needed. | Heat-sensitive materials, mixed-material work, or coated parts where thermal damage is a concern. |
| Oxy-Fuel Cutting Machine | Preheats steel and uses an oxygen jet to oxidize and remove the metal along the cut path. | Primarily carbon and low-alloy steel; generally unsuitable for stainless steel and aluminum using standard oxy-fuel cutting. | Can cut thick steel plate and is often used for heavy-duty work. | Slower and less precise than many sheet-cutting processes; requires heat control and suitable material chemistry. | Extensive heat, flame, and scale can destroy nearby coating. Remove coating in the cutting zone and plan for edge preparation and refinishing. | Thick carbon-steel plate and heavy fabrication. |
| CNC Router | Moves a rotating cutting bit along programmed paths to remove material by machining. | Wood, plastics, composites, and selected nonferrous materials, depending on tooling and machine rigidity. | Flexible for two-dimensional profiles, pockets, and detailed shapes; programs can be reused for repeat parts. | Tool wear, cutting forces, and dust or chips must be managed. Not the usual choice for heavy steel plate. | Clamping and chip contact can scratch coating; the cutting bit removes the coating along the tool path. Use protective workholding where finish matters. | Panels, signage, plastics, composites, and light-duty nonferrous work. |
| Abrasive Cut-Off Saw | Rotates an abrasive wheel against the workpiece to remove material through friction and abrasion. | Metal bars, rods, tubes, and sections compatible with the saw, wheel, and workholding. | Simple method for straight cuts on stock lengths; useful for repetitive cutoff tasks. | Produces a kerf and may generate heat, sparks, burrs, and abrasive dust. Accuracy depends on the saw and clamping. | Wheel contact and heat can damage coating near the cut. Secure the part without crushing or scraping finished surfaces. | Cutting stock to length before machining or assembly. |
| Mechanical Guillotine Shear | Uses a moving blade and a fixed blade to shear sheet metal in a straight line. | Sheet metals within the shear’s rated material type, thickness, width, and strength limits. | Fast, efficient straight cuts in sheet; avoids the heat input associated with thermal cutting. | Limited to straight-line cuts and rated sheet capacity; blade condition and material support affect cut quality. | Blade contact and sheet movement may scratch or chip the finish. Use suitable surface protection and inspect cut edges for coating damage. | Repeated straight cuts in sheet-metal production. |
Important: There is no universal thickness or speed rating for these machine types. Verify the machine’s rated capacity for the exact material and thickness, and test the cutting process on coated parts before full production. Cutting commonly exposes bare material at the edge; corrosion protection or coating touch-up may be required.