Choosing an Air Liquid Spray Nozzle is a technical decision, not a catalog exercise. The correct nozzle must match liquid viscosity, flow rate, air pressure, spray angle, droplet size, and operating temperature. A mismatch can create uneven coating, excessive overspray, clogged passages, or wasted compressed air.
The stakes are practical. The U.S. Environmental Protection Agency’s AP-42 technical compilation connects spray processes with particle formation, capture efficiency, and emissions performance. The European Commission’s Best Available Techniques reference documents also emphasize transfer efficiency and process control in industrial coating operations. Meanwhile, Grand View Research’s spray nozzle market analysis identifies manufacturing, chemical processing, food production, and agriculture as major application areas. These reports show why nozzle selection affects both product quality and operating cost.
Arthur H. Lefebvre, a leading authority on atomization, wrote, “Atomization is the process of breaking up a bulk liquid into droplets.” His statement remains central to every Air Liquid Spray Nozzle evaluation. Droplets tell the story. Smaller droplets may improve coverage, yet they can drift, evaporate, or increase air consumption. Larger droplets may reduce drift, but they can produce weak coverage and visible runs. Nozzle charts help, but they are not perfect. Real liquids behave differently from test fluids. This guide examines spray pattern, atomization quality, material compatibility, maintenance needs, and measurable performance. It also questions common assumptions, because the cheapest nozzle is rarely the lowest-cost choice over time.
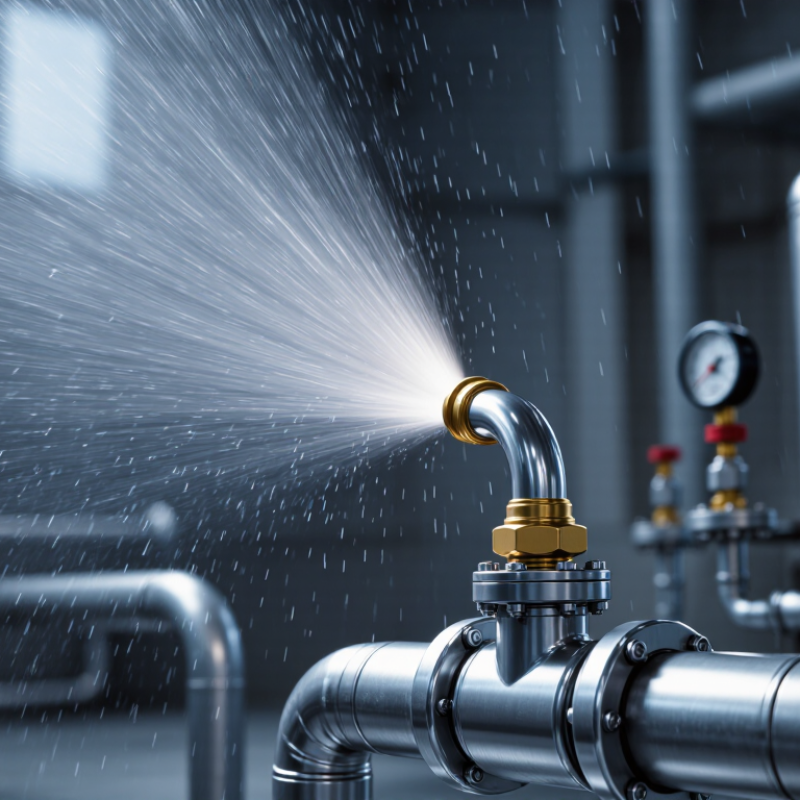
Choosing an air-liquid spray nozzle starts with measurable performance, not appearance. In field testing, SMD, or Sauter Mean Diameter, shows average droplet size by volume and surface area. Smaller droplets can improve evaporation and surface contact, but they may drift more easily. Larger droplets often provide better penetration and reduce airborne loss. SMD is not a universal target. Liquid viscosity, pressure, and air-to-liquid ratio can change it.
Flow rate determines how much liquid reaches the target each minute. Check liquid delivery and compressed-air consumption at operating pressure. A nozzle matching its catalog value may perform differently after tubing, filters, or temperature changes. Spray angle defines cone width at a measured distance. A 60-degree pattern at 100 millimeters differs from one measured at 300 millimeters. Coverage depends on angle, distance, overlap, and target shape. Test a water pattern on the actual surface. This often reveals gaps.
Tips: Record SMD, flow rate, pressure, angle, and coverage on one test sheet. Keep nozzle distance fixed. Inspect the edges. If the center becomes too wet, reduce overlap before increasing pressure. That adjustment may save liquid, but verify it carefully. Quick bench tests can mislead when production liquid behaves differently. Recheck with its actual viscosity and temperature. Selection should remain evidence-based, even when a small compromise seems convenient.
| Metric | Definition and Unit | Indicative Engineering Range | What the Value Indicates | Selection Considerations |
|---|---|---|---|---|
| Sauter Mean Diameter (SMD) | The diameter of a spherical droplet having the same volume-to-surface-area ratio as the complete spray. Usually reported in micrometres (µm). |
Fine atomization: approximately 20–80 µm Medium atomization: approximately 80–200 µm Coarser atomization: typically above 200 µm |
Lower SMD generally provides more surface area, faster evaporation, and better coating or cooling uniformity. It can also increase drift and overspray. | Choose a lower SMD for evaporation, humidification, and fine coating. Choose a larger SMD when penetration, reduced drift, or reduced dusting is more important. |
| Liquid Flow Rate | The volume of liquid delivered per unit of time, normally expressed in L/min, mL/min, or gal/min. | Compact air-liquid nozzles commonly operate from about 0.05 to 5 L/min per nozzle, depending on the liquid cap, pressure, viscosity, and orifice size. | Determines dosing capacity, wetting rate, residence time, and the number of nozzles required for a process. | Select the nozzle near the middle of its stable operating range rather than at its maximum capacity. Confirm the flow using the actual liquid density, viscosity, and temperature. |
| Air Consumption | The compressed-air volume used by the nozzle, commonly stated as normal litres per minute (NL/min) at a specified air pressure. | Many small air-atomizing nozzles use approximately 10–200 NL/min, although larger systems can require substantially more. | Higher air consumption can produce finer droplets and greater spray momentum, but increases compressor capacity, operating cost, and noise requirements. | Check total air demand for all nozzles, peak compressor capacity, line pressure losses, filtration, and available air quality. |
| Spray Angle | The included angle of the spray pattern, measured at a defined distance and operating condition. It is expressed in degrees (°). | Common air-liquid spray angles range from approximately 15° to 120°, depending on whether the pattern is narrow, wide, round, or flat. | A wider angle covers more area at a short distance but may reduce impact intensity and increase the risk of edge-thickness variation. | Match the angle to the target width, nozzle-to-surface distance, overlap, and required impact or penetration. |
| Spray Coverage |
The wetted or treated width on the target surface. For an ideal full-cone pattern, width can be estimated as:
W = 2 × D × tan(θ/2) where D is distance and θ is spray angle. |
Ideal geometric width at 300 mm distance: 30° ≈ 161 mm 60° ≈ 346 mm 90° ≈ 600 mm 120° ≈ 1,039 mm |
The calculated width is theoretical. Actual coverage is affected by spray pattern quality, droplet momentum, air movement, surface angle, and liquid properties. | Use measured spray-pattern data when uniformity is critical. Include an overlap allowance when installing multiple nozzles. |
| Liquid Pressure | The pressure supplied to the liquid inlet, normally measured in bar or psi. | A typical operating window for many air-liquid nozzles is approximately 0.5–7 bar liquid pressure, but the allowable range is nozzle-specific. | Increasing liquid pressure generally increases flow rate and can change droplet size, pattern stability, and operating point. | Avoid selecting a nozzle that requires excessive pressure to meet the target flow. Consider pump capacity, pulsation, and pressure regulation. |
| Atomizing-Air Pressure | The compressed-air pressure used to break the liquid into droplets, normally measured in bar or psi. | Many industrial air-atomizing designs operate around 1–7 bar air pressure, subject to nozzle geometry and the required SMD. | Higher air pressure usually improves atomization and spray momentum but raises air consumption and may increase overspray. | Set air pressure high enough to achieve the required droplet size and pattern, but not higher than necessary for the process. |
| Liquid Viscosity | The liquid's resistance to flow, generally reported in mPa·s or cP. | Water-like liquids are close to 1 mPa·s at room temperature. Liquids above approximately 20–50 mPa·s often require higher air pressure, larger passages, or specialized nozzle designs. | Higher viscosity generally makes atomization more difficult and can increase SMD while reducing flow stability. | Specify viscosity at operating temperature, not only at room temperature. Also check solids content, surface tension, and filtration requirements. |
| Spray Pattern | The geometric distribution of droplets, such as round, full cone, hollow cone, flat fan, or elliptical pattern. | Pattern selection is application-dependent; flat fan patterns suit strips and sheets, while round or cone patterns suit localized three-dimensional targets. | Pattern geometry affects overlap, edge deposition, impact distribution, and the number of nozzles needed. | Select the pattern according to the target shape and motion. Validate uniformity across the complete operating pressure range. |
| Recommended Application Fit | A practical comparison of common process objectives and preferred nozzle characteristics. |
Evaporation or humidification: low SMD, high air assistance Coating: controlled flow, uniform coverage Cooling: moderate SMD, stable pattern Dust suppression: larger droplets, lower drift |
No single nozzle setting is optimal for every process. The best choice balances droplet size, liquid capacity, coverage, air use, and drift control. | Test the nozzle with the actual liquid and target surface. Compare SMD, flow rate, coverage uniformity, air consumption, and operating cost together. |
How to Choose an Air Liquid Spray Nozzle?
Choosing an air liquid spray nozzle starts with the liquid, not the nozzle catalog. Viscosity controls how easily liquid travels through the orifice. Thin liquids often atomize with less air pressure. Thick liquids may need a larger passage and stronger air assistance. Test the liquid at its actual operating temperature. A sample that pours easily at room temperature may spray poorly beside a heated process line.
Surface tension also changes droplet formation. High surface tension can produce larger droplets, uneven coverage, or liquid tails. Adjusting air pressure may help, but excessive air can create overspray and wasted material. Suspended solids require special care. Measure particle size, concentration, and settling behavior before selecting an orifice. A narrow opening may clog quickly. A larger opening can reduce blockage, though it may alter spray coverage. Temperature deserves equal attention because it affects viscosity, evaporation, seals, and worker safety.
Tips: Record viscosity, temperature, solids content, and surface tension during a real trial. Watch the spray pattern for several minutes, not only at startup. Clean the nozzle after testing and inspect the orifice under magnification. Laboratory results can mislead when the production line vibrates or the liquid warms unevenly. Do not rely on pressure readings alone. Compare droplet appearance, coverage, flow rate, and clogging frequency. Sometimes the “best” nozzle is only acceptable, and a second trial exposes that weakness.
Match the nozzle to viscosity, surface tension, solids content, and operating temperature. Higher viscosity usually requires a larger liquid orifice and higher atomizing energy, while suspended solids require passages that resist plugging. Lower surface tension generally improves atomization and spray spreading.
Representative liquid-property values at approximately 20°C. Actual values vary with formulation, temperature, and measurement method.
Choosing an air liquid spray nozzle starts with the required droplet size, not the nozzle shape. A 10–30 μm spray creates a fine mist with rapid evaporation. It can suit humidification, coating, and controlled cooling. However, very small droplets drift easily and may miss the target.
Droplets between 30 and 80 μm often provide a practical balance. They spread across surfaces while remaining less sensitive to light air movement. For cleaning, lubrication, or moderate cooling, this range may be easier to control. Larger droplets, around 80–200 μm, carry more liquid and resist evaporation. They can work better on moving surfaces or where wetting matters. Think about the target first.
Air pressure, liquid pressure, viscosity, and flow rate all change atomization performance. Higher atomizing air pressure usually produces finer droplets, but it also increases energy use and noise. Thick liquids may need wider passages or more air assistance. Test the nozzle with the real liquid, temperature, and operating pressure. A water test is useful, but it can mislead. Measure droplet distribution with suitable equipment instead of trusting appearance alone. In field trials, I would record spray width, wetting pattern, overspray, and liquid consumption. Conditions rarely stay perfect. A nozzle that performs well in a laboratory may produce uneven coverage beside a fan or conveyor. Allow adjustment, and question results that seem too convenient.
Choosing an air liquid spray nozzle begins with supply sizing, not the nozzle catalog. At 1–7 bar, air pressure strongly affects atomization, coverage, and operating noise. Liquid flow depends on pressure, viscosity, density, and orifice size. Record each value at the nozzle inlet, not only at the compressor or pump. A 1 bar reading at the source may become much lower after filters, hoses, and regulators.
The U.S. Department of Energy reports that compressed-air leaks can waste 20–30% of compressor output. This loss can distort nozzle testing. The same pressure setting may produce weaker spray during peak factory demand. CAGI guidance also emphasizes measuring flow, pressure, and pressure drop across the complete air system. Keep the air line short and generously sized. Then verify actual consumption with a calibrated flow meter. Small details matter.
For liquid sizing, begin with the required flow rate and spray pattern. A finer droplet usually requires more atomizing air or a smaller liquid passage. However, excessive air can create rebound, mist, and uneven coating. At 1–7 bar, test several pressure points, such as 2, 4, and 6 bar. Record droplet appearance on the target surface. ISO 8573-1 classifications remind users that oil, water, and particles can affect process air quality. Clean air helps, but it does not fix poor sizing. I would not trust a theoretical chart alone. Temperature changes and fluid batches can quietly shift results. Some testing must be imperfect before it becomes useful.
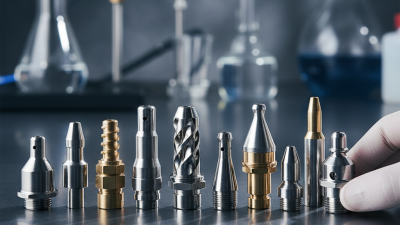
Selecting an air liquid spray nozzle starts with the material, not the catalog photo. Confirm the liquid’s chemistry, temperature, viscosity, and solid content. Stainless steel suits many industrial fluids, while harder inserts may resist abrasive particles better. Seals also matter. A compatible body can still fail when its seal swells or cracks. Request documented material data, and compare it with your actual operating conditions.
Wear life should be checked through inspection records and controlled testing. Look for changes in spray angle, droplet pattern, and flow rate. Small orifices can wear faster than expected.
Air consumption is equally practical. Measure pressure and airflow at the nozzle, then compare them with compressor capacity. Excessive air use can increase noise, energy costs, and unstable atomization. The estimate is rarely perfect.
Tips: Test one nozzle under real production conditions before wider installation. Record liquid temperature, pressure, air usage, and operating hours. Check the spray pattern at the target distance. Also verify application compliance, including hygiene, worker exposure, electrical-area restrictions, and local equipment requirements. A nozzle suitable for coating may be unsuitable for food contact or sensitive cleaning processes. Do not rely only on supplier claims. Keep the test data. Recheck it after maintenance, because field conditions often differ from the original design.